


How to Choose the Right Biochar Production Equipment for You?
Oct 23, 2026
How to Choose the Right Biochar Production Equipment for You?
Choose biochar production equipment by defining the product you need, the feedstock you can reliably supply, and the conditions the complete line must maintain. Compare suppliers using the dry biochar that meets your agreed specification and the utilities needed to produce it.
A large reactor can still be the wrong purchase when drying, feeding, or cooling limits production. Useful capacity is the rate of acceptable product leaving the whole plant under your operating conditions.
Define the biochar you need to sell
Write a product specification before requesting a reactor quotation. Soil amendment, filtration media, and industrial carbon applications need different properties, so a high carbon percentage alone cannot establish suitability.
Discuss the required particle size, ash, pH, contaminants, and application performance with potential buyers. Add the relevant laboratory methods and reporting basis so that competing samples can be compared consistently.
Keep fixed carbon, organic carbon, and stability separate. Fixed carbon is a proximate-analysis result; it does not establish organic-carbon content or long-term persistence. A high mass yield also says little about whether the product meets its intended specification.
Agree on product acceptance criteria before choosing the temperature, heating arrangement, or capacity.
Specify the feedstock you can supply
Sample the biomass across its expected supply variation, including seasonal changes. A trial on clean, dry material cannot establish performance on a wetter or more contaminated supply.
Measure the properties that affect operation
Record moisture with its wet or dry basis, particle-size distribution, bulk density, ash, contaminants, and flow behavior. These affect the preparation equipment and the material entering the reactor.
Fine or low-density material may require densification. Oversized pieces may need crushing or screening, while wet feed can add a drying load. Confirm preparation requirements through material tests.
Match capacity to reliable supply
Base the supply estimate on biomass you can collect, store, and deliver consistently. Include transport distances, competing uses, and seasonal storage requirements.
An oversized continuous line can spend too much time waiting for feedstock. Give suppliers the expected material range and operating calendar, then ask them to identify any conditions that require reduced throughput or additional preparation.
Match the process to your product and schedule
Intermittent biomass supply and continuous factory production call for different operating plans. Batch equipment can suit intermittent duties, but its output calculation must include loading, heating, cooling, and unloading. Continuous systems need dependable feed preparation, staffing, and maintenance support.
Choose the thermal route
For a project considering continuous rotary kilns, use the target product and process requirements to narrow the options.
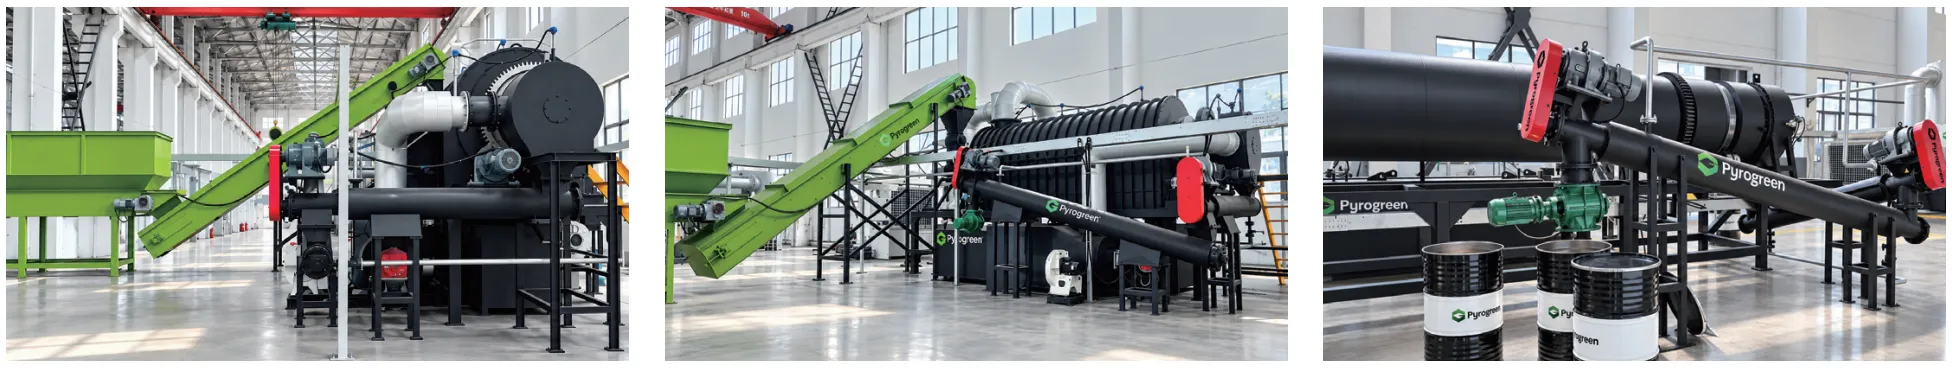
Pyrogreen's biochar production equipment uses continuous rotary kilns for its listed carbonization and torrefaction routes.
| Route | Suitable project objective | What to verify |
| Indirectly heated rotary pyrolysis | Biochar or biocarbon requiring control of processing conditions | Heat transfer, residence time and product properties on the proposed feedstock |
| Autothermal continuous carbonization | Continuous industrial biochar production across a broader throughput range | Prepared-feed requirements, combustion control and fuel demand across operating conditions |
| Rotary torrefaction | Biocoal or torrefied biomass for fuel upgrading | Whether the intended fuel specification matches this product route |
Torrefaction serves a different product objective from conventional biochar production. Autothermal operation also requires an energy balance before any claim of fuel independence is credible.
Check how the line will operate
Review startup frequency, minimum operating rate, shutdown procedures, and maintenance access. Identify who will operate each shift and how quickly critical spare parts can reach the site.
Select the configuration your feedstock supply and operating team can sustain.
Compare capacity on a dry basis
Require quotations to identify whether capacity means incoming wet biomass, dry feed, or finished biochar. Those quantities cannot be compared directly.
Convert incoming biomass consistently
In a hypothetical comparison, two streams each deliver 2.0 t/h of incoming biomass. With moisture at 20% on a wet basis, one contains 1.6 t/h of dry matter; at 50%, the other contains 1.0 t/h.
Dry feed rate = incoming biomass rate × (1 − wet-basis moisture fraction).
Equal wet throughput therefore carries different dry conversion duties. This calculation does not establish that a particular machine can maintain the same incoming rate at both moisture levels.
Calculate acceptable output
Request dry-basis biochar yield measured at the operating conditions that produced an acceptable sample. Apply that yield to the dry feed rate, then account for any material failing the agreed product specification.
For annual output, use a realistic operating calendar and maintenance allowance. If the operating hours already exclude downtime, do not deduct it again through an availability factor. Compare offers using the same feed and product basis.
Price the complete line and its energy demand
Obtain a quotation covering every required step from biomass reception to cooled, collected product. A reactor price cannot establish the investment needed to operate a plant.
Define the supply boundaries
Identify who supplies drying and sizing equipment, storage, conveyors, feeders, gas treatment or combustion, cooling, controls, and product handling. Clarify responsibility for civil works, utilities, installation, commissioning, training, and spare parts.
Cooling also affects saleability. Biochar exposed to pyrolysis gases containing polycyclic aromatic hydrocarbons (PAHs) during cooling can collect these contaminants through condensation or adsorption. Check gas–char separation and sample the finished product after the relevant cooling and handling steps.
Count energy that can actually be used
Separate startup fuel, steady-operation fuel, auxiliary electricity, and internal drying demand. Count exported heat only after internal loads and losses, and only where a suitable heat user exists. The same gas energy cannot be fully allocated to drying and sold again as exported energy.
Compare operating costs per dry tonne meeting the product specification, using consistent assumptions for labor, maintenance, and utilities. Keep uncertain carbon revenue separate from the base case, and require a mass-and-energy balance before accepting energy-saving claims.
Require evidence before placing the order
Make representative-feedstock testing part of supplier evaluation. Connect throughput, product results, and utility measurements to the same documented operating conditions.
Agree on measurable acceptance conditions
Define the test material, duration, sampling methods, and treatment of interruptions before the trial. Choose a duration suited to the process; a short demonstration cannot prove annual availability.
| Acceptance item | Evidence to request |
| Feed and capacity | Measured feed rate, moisture basis, size range and preparation requirements |
| Operating conditions | Recorded reactor temperatures and residence conditions linked to the sampled product |
| Qualified product | Dry char mass, representative samples and agreed laboratory results |
| Utilities and energy | Fuel, electricity, internal heat use and any measured useful export | |
| Emissions and safety | Applicable emissions testing, gas-management arrangements and checks of shutdown protections |
| Operability and service | Operator duties, cleaning access, maintenance schedule and critical-spares plan |
Plan quality and carbon records
If carbon removal is part of the project, choose the intended methodology and storage pathway before specifying instruments and recordkeeping. Weighing, moisture measurements, sampling, energy records, and traceability need to support that pathway.
Equipment pre-approval, product certification, and project credit issuance are separate evaluations. Local permits also remain site-specific. Require the supplier to state which documents and monitoring functions are included, and which remain the project's responsibility.
Send suppliers the same specification
Prepare one request for quotation that describes the feedstock range, target product, production schedule, site utilities, and acceptance conditions. Ask each bidder to list deviations and exclusions against that document so the remaining trade-offs are visible.
Before signing, agree in writing how changes will be handled. A new biomass supplier, different particle size, or revised product market may require another trial, added preparation, or a revised operating limit.
Define who approves the change and who pays for the necessary work. A purchase agreement that addresses these changes gives the plant a clearer path through its first supply disruption or product adjustment.
CONTACT US
Contact US
Product Information
Quantity
Unit
Piece
Support order samples, customization, wholesale direct, and complete payment. If the product you look for does not have corresponding customized content, pls fill out the form below to contact us, and we will reply ASAP.